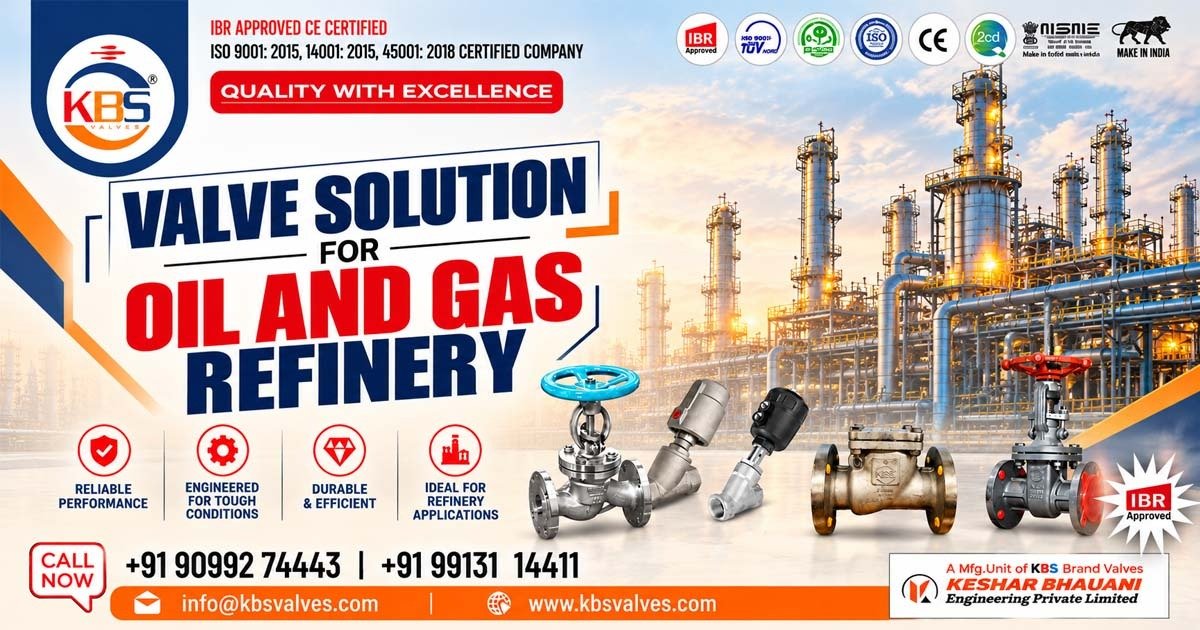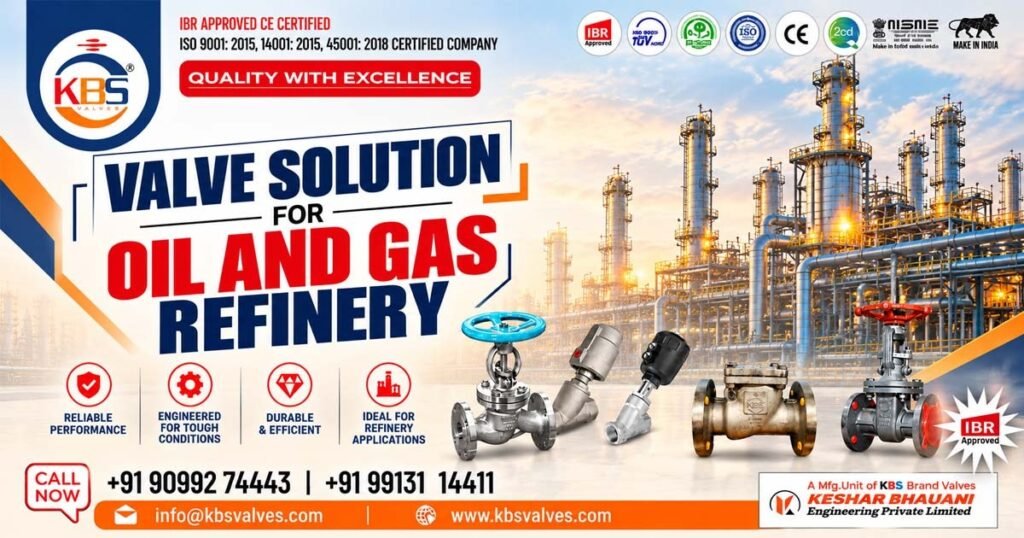
KBS Valves: A Trusted Valve Manufacturer for Oil & Gas Refineries
Refineries run on pressure, heat and aggressive media, so a valve failure means shutdowns, safety risk and lost revenue.
KBS Valves engineers industrial valves for these conditions, with a focus on leak-tight sealing, long service life and consistent quality.
Why Refineries Choose KBS Valves
- Severe-service engineering: designed for high-pressure, high-temperature and corrosive hydrocarbon environments.
- Tight shut-off performance: precision machining and seat design for reliable sealing.
- Material versatility: carbon steel, alloy steel, stainless steel and duplex options for different process media.
- Lower lifecycle cost: durable build reduces unplanned downtime and replacement frequency.
- Application-based selection: valves matched to the process, not just the catalogue.
Valve Range for Refinery Applications
- Gate Valves: full-bore isolation for crude, product and utility lines.
- Globe Valves: precise throttling and flow regulation.
- Check Valves: backflow prevention to protect pumps and compressors.
- Ball Valves: quick shut-off with low torque and minimal leakage.
- Butterfly Valves: compact, cost-efficient control for large-diameter lines.
Quality & Compliance Standards That Matter
- Design and testing aligned with industry benchmarks such as API 600, API 602, API 6D, API 598, ASME B16.34 and ISO 9001.
- Material traceability with test certificates.
- Pressure, hydrostatic and seat leakage testing before dispatch.
- Third-party inspection support on request.
- NACE-compliant material options for sour service.
Where KBS Valves Perform Best in a Refinery
- Crude distillation units (CDU/VDU).
- Fluid catalytic cracking (FCC) and hydrocracking.
- Hydrotreating and desulphurisation units.
- Storage, tank farms and pipeline transfer.
- Steam, cooling water and utility systems.
How to Choose the Best Valve Manufacturer for Oil & Gas Refineries
- Check certifications and testing capability.
- Verify material range and traceability.
- Ask for proven refinery or petrochemical references.
- Confirm customisation and engineering support.
- Evaluate delivery timelines and after-sales service.
Frequently Asked Questions
Q1: Which valve manufacturer is best for oil and gas refineries?
A1: The best manufacturer combines API-standard design, severe-service materials, rigorous testing and proven refinery experience. KBS Valves is built around these criteria.
Q2: Which valves are most used in refineries?
A2: Gate, globe, check, ball and butterfly valves, chosen by pressure, temperature and media.
Q3: What materials suit corrosive refinery service?
A3: Alloy steel, stainless steel and duplex grades, with NACE-compliant options for sour service.
Q4: Which standards should refinery valves meet?
A4: Typically API 600, API 602, API 6D, API 598 and ASME B16.34.
Q5: How do I request a quote from KBS Valves?
A5: Share your valve type, size, pressure class, material and media details with the KBS Valves team for a technical quotation.
We Supply Best Valve Manufacturer for Oil and Gas Refineries in Karnataka including locations Bangalore, Mysore, Hubballi-Dharwad, Kalaburagi, Mangalore, Belagavi, Davanagere, Bellary, Vijayapura, Shimoga, Tumkur, Raichur, Bidar, Udupi, Hospet, Gadag-Betageri, Robertsonpet, Hassan, Bhadravati, Chitradurga, Kolar, Mandya, Chikmagalur, Gangavati, Bagalkot, Ranebennuru, and Arsikere.
Ready to secure refinery uptime? Request your KBS Valves technical quote today and engineer leak-free performance.
- Website: www.kbsvalves.com
- Email: info@kbsvalves.com
- Phone: +91 90992 74443 | +91 99131 14411
View Product: Click here